CONCEPT
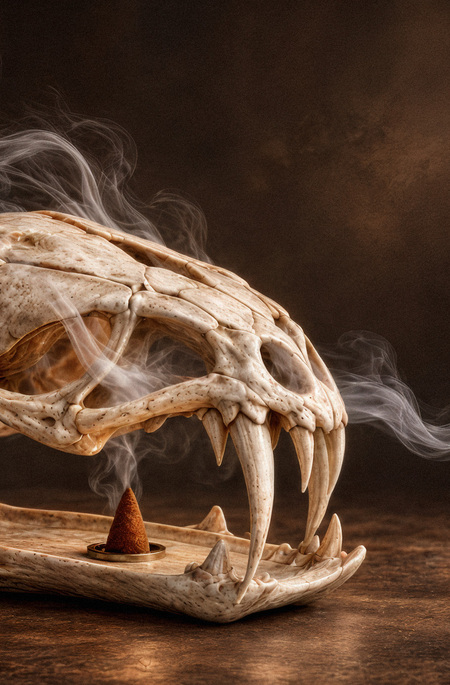
The tabletop censer, shaped like a skull, reinterprets the myth of winged serpents that guarded frankincense trees. According to legend, smoke was used to ward off creatures and gain access to the incense.
In this project, the narrative is inverted: the smoke becomes part of the amphipteron’s image, passing through the hollow skull to create the effect of its «breathing.»
MANUFACTURING TECHNOLOGY
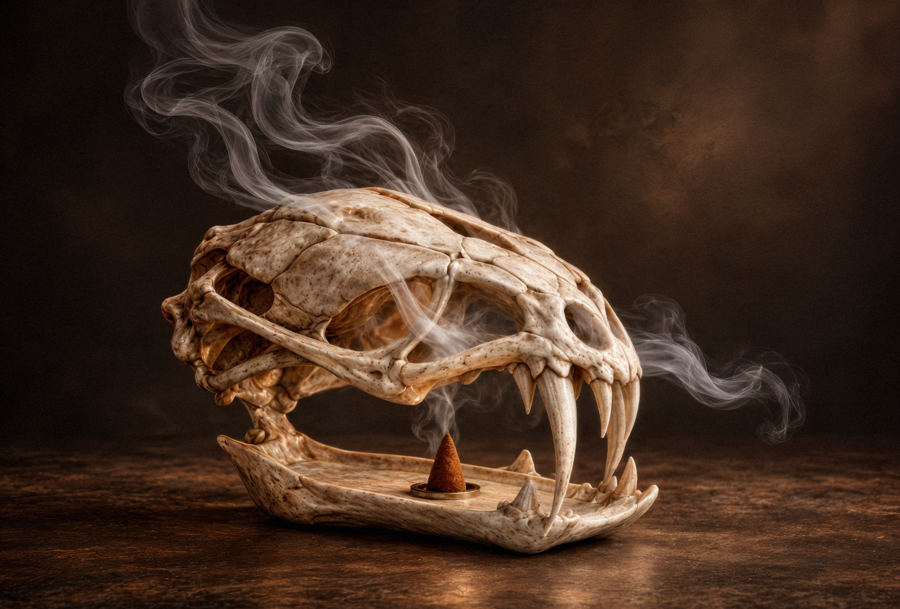
The object is a two-part 3D-printed ashtray, consisting of the upper skull portion and the lower jaw-base.
1. Two-part 3D printing—the upper skull section and the lower jaw-base are printed separately. 2. Assembly of the structure—the parts are fitted together, forming a semi-open skull position. 3. Priming and surface preparation—print marks are removed, the surface is leveled, and primed. 4. Painting and lacquering—a bone tone is applied, followed by a matte protective varnish. 5. Installation of the heat-resistant insert—a metal base for the aromatic cone is installed into the lower jaw.
Point 1. 3D Printing
The details are printed using the FDM method from PETG plastic with a 0.4 mm nozzle. The upper skull and lower jaw are manufactured separately, utilizing technical supports for complex overhangs.
Point 2. Assembly
The upper skull is fitted onto a connecting pin located on the lower jaw and secured in a defined semi-open position. The pin is printed simultaneously with the lower jaw as part of a single piece, and a corresponding receptacle is provided on the upper skull.
Step 3. Priming and Surface Preparation3D-printed marks are sanded with sandpaper, followed by the application of an acrylic primer-filler, and the surface is sanded again until smooth.Step 4. Painting and VarnishingAn ivory-toned acrylic paint is applied, and the depressions are tinted with a darker acrylic paint to emphasize the relief. Finally, the object is coated with a glossy acrylic varnish.Step 5. Installing the Heat-Resistant InsertThe lower jaw is designed with a seating recess for the finished metal insert for the aromatic cone. A stainless steel insert with a diameter of approximately 30 mm is used. The seating area is designed with a small technical clearance and a depth of about 4 mm. The finished insert is purchased separately and secured in the base with a heat-resistant adhesive compound.